Before production
Include fixture design, manufacturing, component sourcing and setup preparation.

Workholding affects part quality, setup time and how much productive work your machine can complete. A well-planned fixture makes a difference throughout the job, from loading the first workpiece to preparing the next order.

A part must be located, supported and clamped before machining can begin. The fixture also affects tool access, unloading, cleaning and preparation for the next job.
Repeated adjustments, awkward loading or unnecessary repositioning add work to every batch. Improving the fixture layout can reduce these steps and help you get more from the machines and people already in your production.
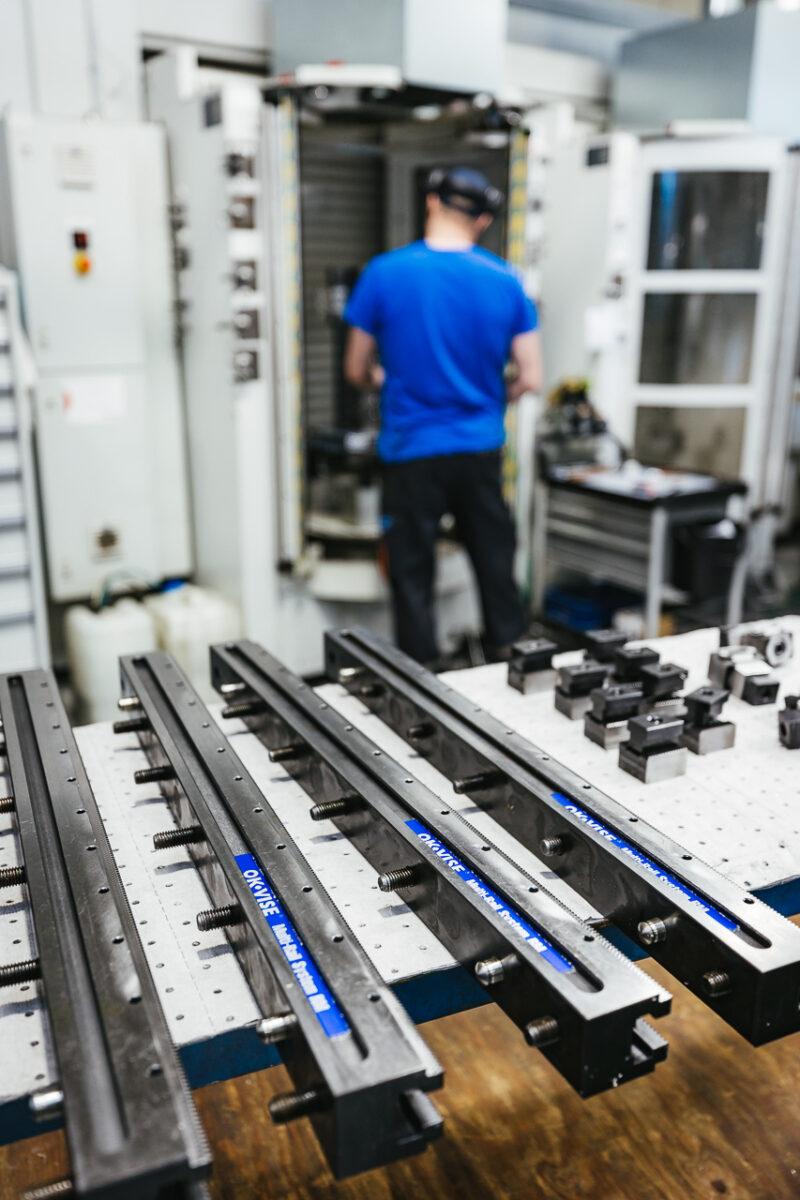
Repeatable locating and suitable support help control workpiece movement and deflection. Clamping force matched to the part helps hold it securely without unnecessary distortion.
Keep clamps and supports clear of the surfaces being machined. Suitable layouts can reduce repositioning and allow more operations in one clamping.
Simplify loading and changeovers, or hold several workpieces in one setup. Fewer interruptions can leave more time for machining.
Document locating references, component positions and clamping instructions. Clear records reduce repeated decisions and help operators rebuild proven setups.
Plan access for loading, cleaning and tightening. Reducing awkward reaches, repeated lifting and unnecessary handling supports a more manageable working routine.
THE COST OF WORKHOLDING
The cost of a fixture continues after it has been purchased or manufactured. Compare what it takes to prepare, run and repeat the job.
Include fixture design, manufacturing, component sourcing and setup preparation.
Consider loading, cleaning, adjustments, machine stoppages and any workholding-related scrap or rework.
Account for storage, maintenance, modifications and the time needed to find and rebuild the setup.
Start with the steps that repeat most often or cause the greatest disruption in your production.
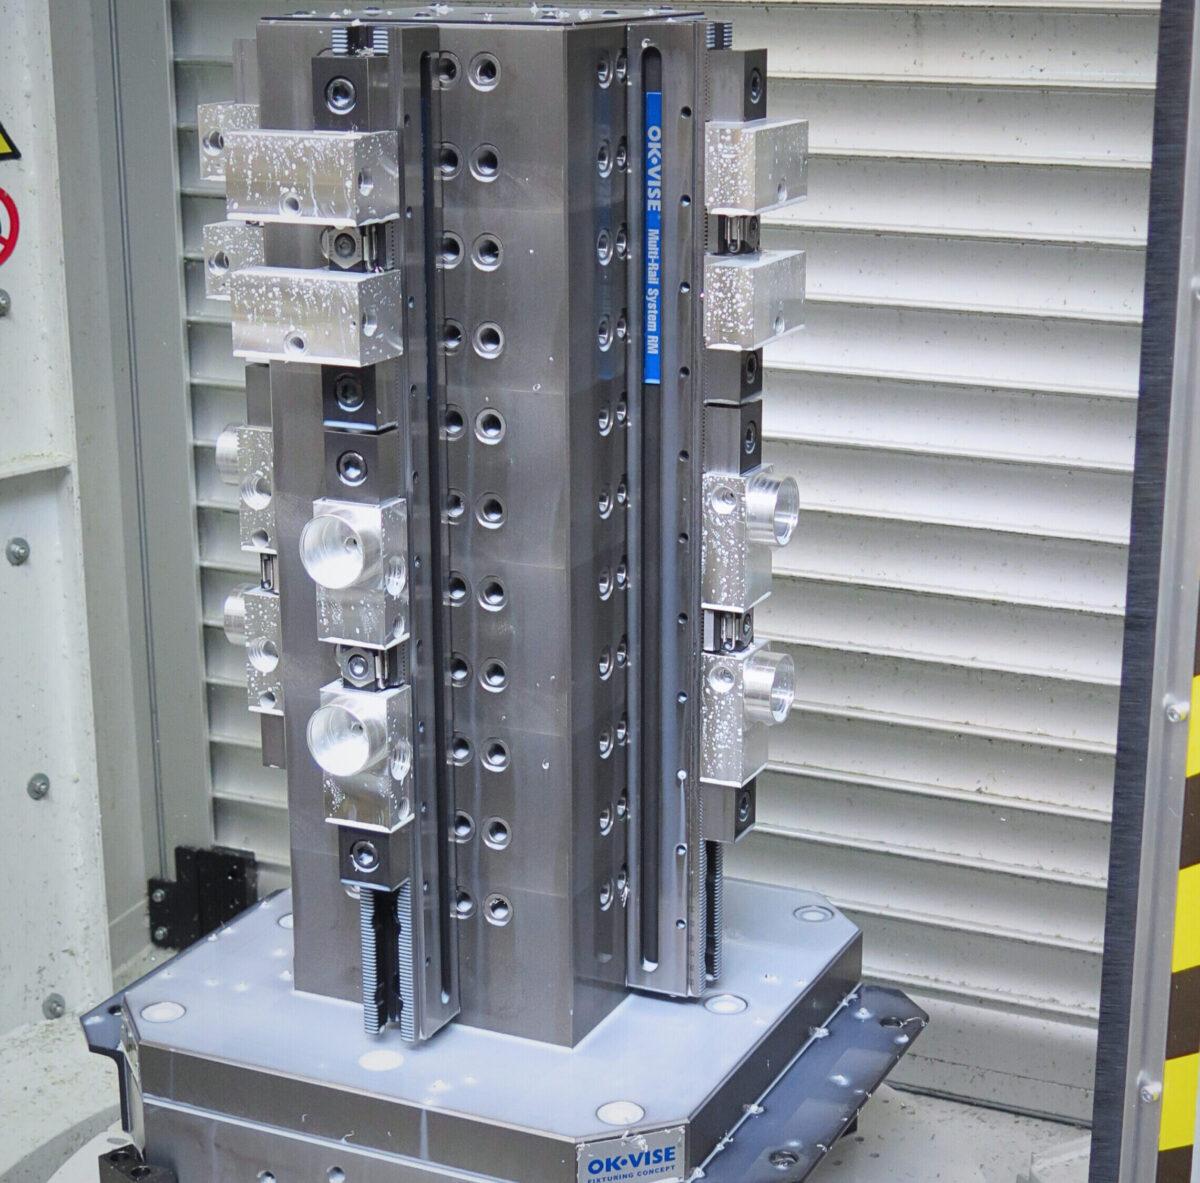
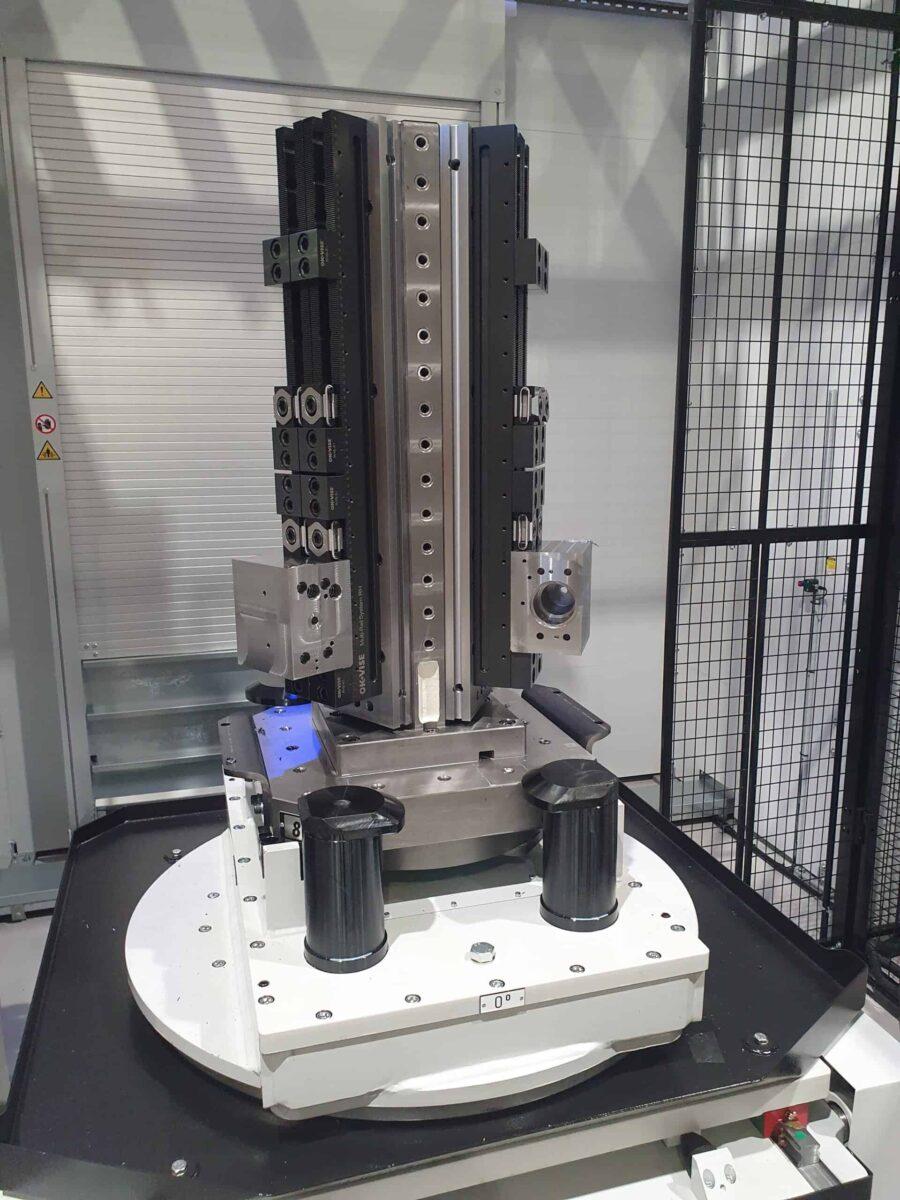
Holding several workpieces lets the machine process more parts before the next loading stop. Where the machining sequence allows, each tool can work across several parts before a tool change. The benefit depends on the complete cycle, including loading effort, tool travel and chip clearance.
Fixture assembly, adjustment and workpiece loading can take place outside the machine when the equipment and workflow support it. This is already an established part of pallet pool and FMS operation. On a stand-alone machine, exchangeable fixture plates can help apply the same principle.
Standard components, clear setup records and organized storage help when similar preparation tasks recur across different jobs. They make existing work easier to reuse and reduce dependence on individual memory. Dedicated fixtures remain useful where the part or production volume justifies them.
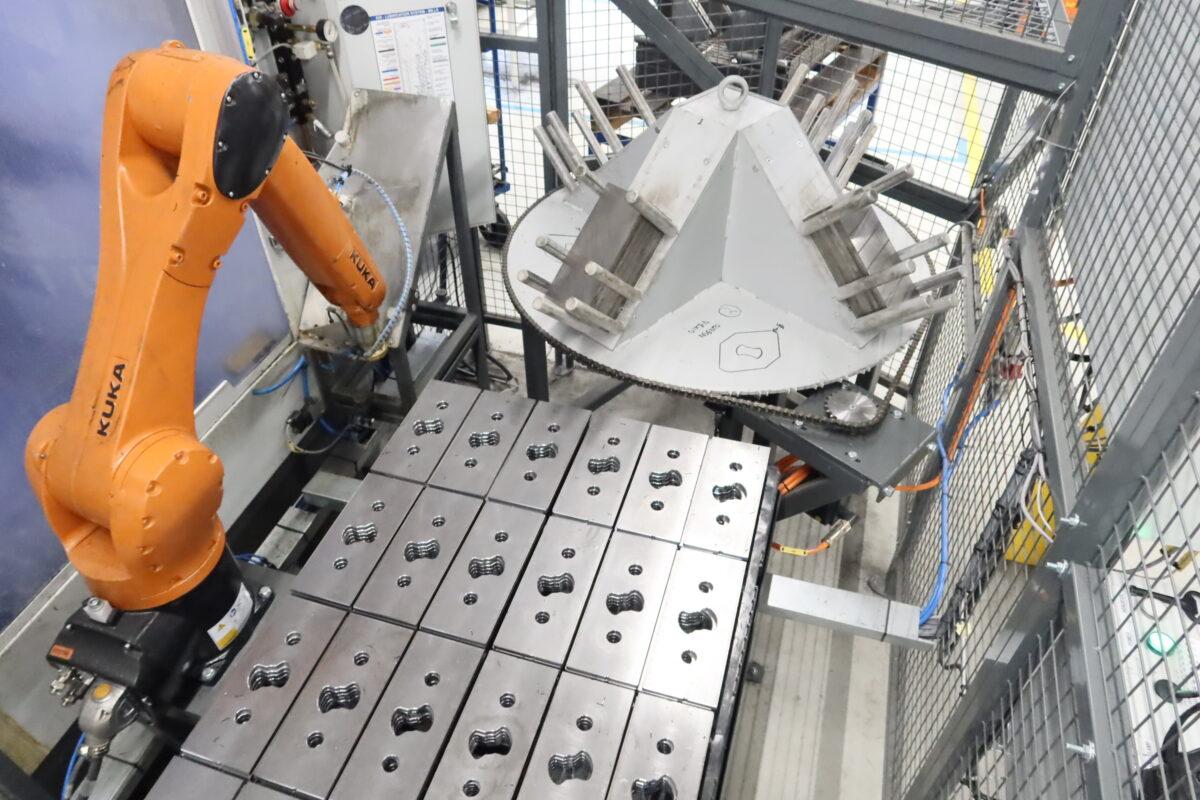
Automated handling relies on consistent workpiece location and a predictable loading and clamping sequence. Workholding needs to be planned together with access, cleaning and process checks. Automatic pallet handling can use manually loaded fixtures; robotic workpiece loading requires a suitable clamping and release method.
APPLICATION IN FOCUS
Check out how OK-VISE has helped its customers.
You can find all our case studies here.
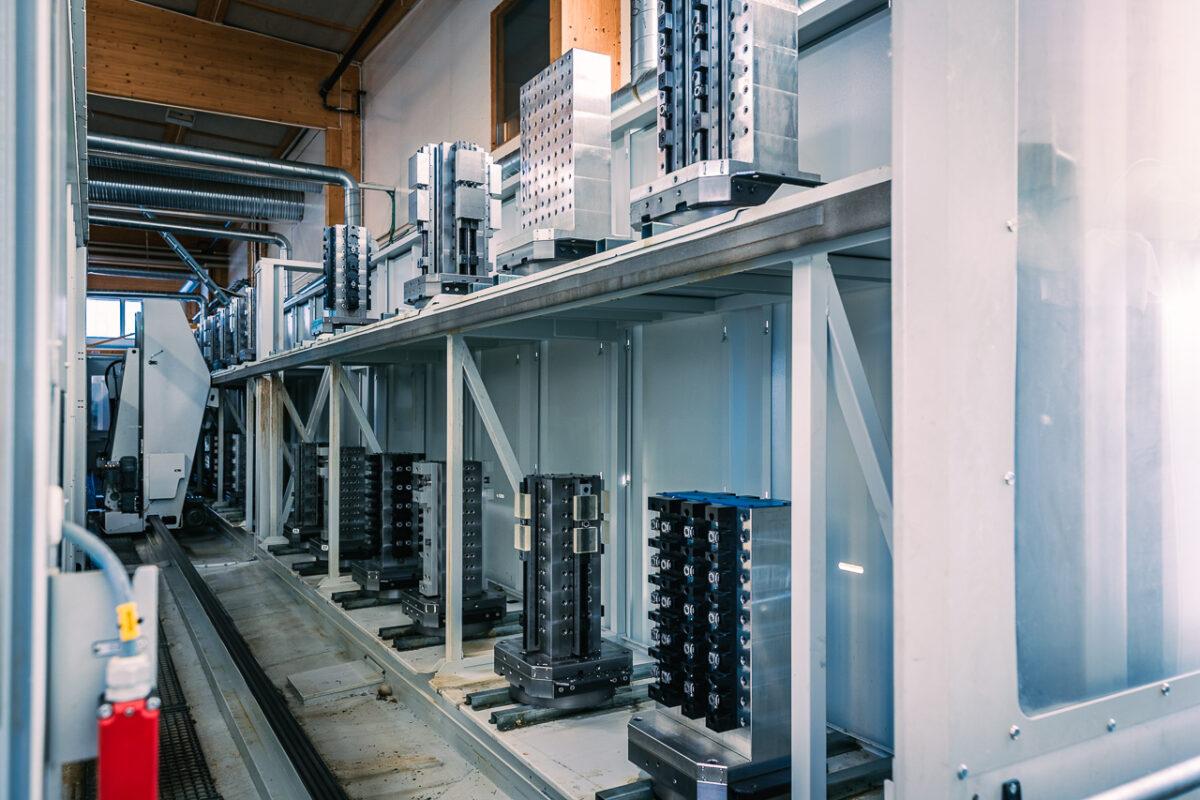
Explore practical approaches for pallet pools and FMS, stand-alone machining centers and high-mix production. See how fixture layouts, reusable components and changeover methods can support the way you work.
DISCUSS YOUR APPLICATION
Tell us about one workpiece, the machine you use and the part of the process that causes delays, extra handling or inconsistent results. We can help assess whether a different workholding arrangement could improve the job.

Prefer local support?
"*" indicates required fields